
Railway braking systems place flexible pneumatic hoses under a duty cycle that differs considerably from road vehicles. Long train formations, repeated coupling movements, vibration from rail joints, and extended maintenance intervals all influence how air brake hose must be specified.
These conditions give a reinforced hose extrusion line a different production focus from equipment intended for conventional commercial vehicle tubing. DEKUMA provides extrusion technology that can be adapted to demanding hose applications, while railway production itself is shaped by durability, dimensional consistency, and certification requirements.
Where Railway Air Brake Hoses Are Used
Inter-vehicle connections represent one of the most visible applications. Brake hoses must bridge the gap between coupled rail vehicles while allowing relative movement during operation. Curves, acceleration, braking, coupling, and uncoupling can all change the hose position, so flexibility must coexist with resistance to repeated mechanical stress.
Locomotive and carriage brake circuits create another application category. Internal routing may expose hoses to vibration, temperature changes, limited installation space, and contact with nearby mechanical components. Unlike a static pneumatic connection, these lines can experience movement throughout their service life, particularly around bogies and other mechanically active areas.
The operating environment also differs from commercial trucks. Railway vehicles can remain in service for long periods and accumulate substantial mileage before scheduled maintenance. Hose specifications consequently need to consider ageing, pressure retention, abrasion, and fatigue over extended service intervals rather than focusing only on initial performance.
Why Railway Pressure Requirements Differ
Rail braking systems rely on carefully controlled pneumatic pressure to coordinate braking across multiple vehicles. Depending on the train architecture, operating pressure, response requirements, and circuit configuration can differ from those found in road vehicles. Tube and hose construction must reflect the actual system parameters rather than being selected solely from general-purpose pneumatic specifications.
Reinforcement helps control dimensional changes when internal pressure fluctuates. Fibre construction, layer arrangement, and reinforcement density influence the hose’s ability to resist expansion while retaining sufficient flexibility. Excessive stiffness can complicate installation and movement, whereas insufficient structural support may affect long-term pressure performance.
Temperature must also be considered alongside pressure. Railway hoses may encounter heat generated by braking equipment, seasonal temperature variation, and localised conditions around mechanical assemblies. Material properties can shift with temperature, so qualification should examine the expected operating range rather than relying on room-temperature measurements alone.
Production Controls for Long-Service Applications
Consistency across the hose length becomes particularly important when products are intended for railway systems. Variations in wall thickness, reinforcement position, or outer diameter can influence bending behaviour and connection quality. Continuous extrusion must consequently maintain stable material flow while keeping multiple process variables within their specified ranges.
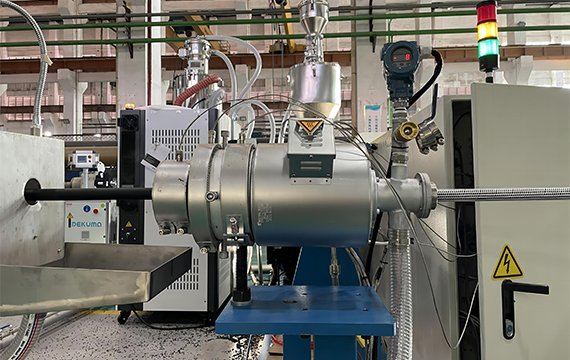
DEKUMA‘s TPV Knitted Reinforced Hose Extrusion Line uses a three-layer structure consisting of a TPV inner layer, knitted polyester or aramid reinforcement, and TPV outer coating. Its configuration can also produce double-layer and single-layer hose constructions. The equipment incorporates controlled inner-layer extrusion, customised fibre reinforcement, and infrared heating to support bonding between the layers during continuous production.
Production speed alone does not define suitability for rail applications. Material residence time, temperature stability, reinforcement tension, cooling conditions, and haul-off synchronization can all influence the finished hose. A stable process window helps manufacturers maintain dimensional repeatability across long production runs where inconsistent sections could complicate downstream inspection.
Certification and Road-Rail Differences
Railway components commonly face application-specific approval and certification requirements set by rail authorities, operators, or applicable standards. The precise requirements vary according to the vehicle type, operating region, braking architecture, and intended service. Documentation and traceability can consequently form an important part of production control alongside physical testing.
Commercial vehicle brake hose standards may address pressure, flexibility, temperature, ageing, and dimensional performance, but railway applications can impose different combinations of tests and service expectations. Rail operators may also require evidence from durability testing, material qualification, production audits, or other conformity procedures before a hose enters operational service.
Testing should reflect realistic railway conditions. Pressure cycling can assess repeated pneumatic loading, while flex-fatigue testing examines mechanical movement. Abrasion, temperature ageing, leakage, burst resistance, and connection retention may provide additional information depending on the specification. Certification is not simply a label applied after manufacturing; it is connected to the documented relationship between material, process, testing, and the final hose design.
Conclusion
Railway air brake hose production sits at the intersection of pneumatic performance, mechanical movement, long service intervals, and formal approval requirements. Inter-vehicle connections demand flexibility during coupling and operation, while locomotive and carriage circuits introduce their own routing and environmental constraints.
DEKUMA’s multilayer extrusion approach illustrates how reinforced hose construction can be configured around different material and reinforcement requirements. Ultimately, a reinforced hose extrusion line paired with a suitable TPV extruder must be evaluated against the specific pressure, fatigue, environmental, dimensional, and certification criteria of the railway application.
